
Capabilities
Cutting and forming
Every weldment starts as flat plate. It is cut on a CNC laser and folded on a CNC press brake in the same hall it is welded in, from the customer's DXF or from our own unfolds.
What it is
A TRUMPF TruLaser 3040 CNC laser with a 2 000 x 4 000 mm bed and 3 200 W cuts plate up to 20 mm thick. Nests are programmed from the DXF the customer supplies or from the unfolds our own office derives from the STEP model, so a hopper cone or a folded housing panel arrives at the brake with its bend allowances already in the flat.
A DURMA AD-S 60400 CNC press brake with 400 t of force, a 6 050 mm table and a 365 mm stroke folds those blanks. Long folds are made in one hit up to the table length; cones, boxes and channels for hoppers, housings and walkway edges are folded in sequence on the same machine.
Cut and formed parts go straight into tacking. Nothing is trucked between subcontractors: the laser, the brake and the welding bays are under one roof.
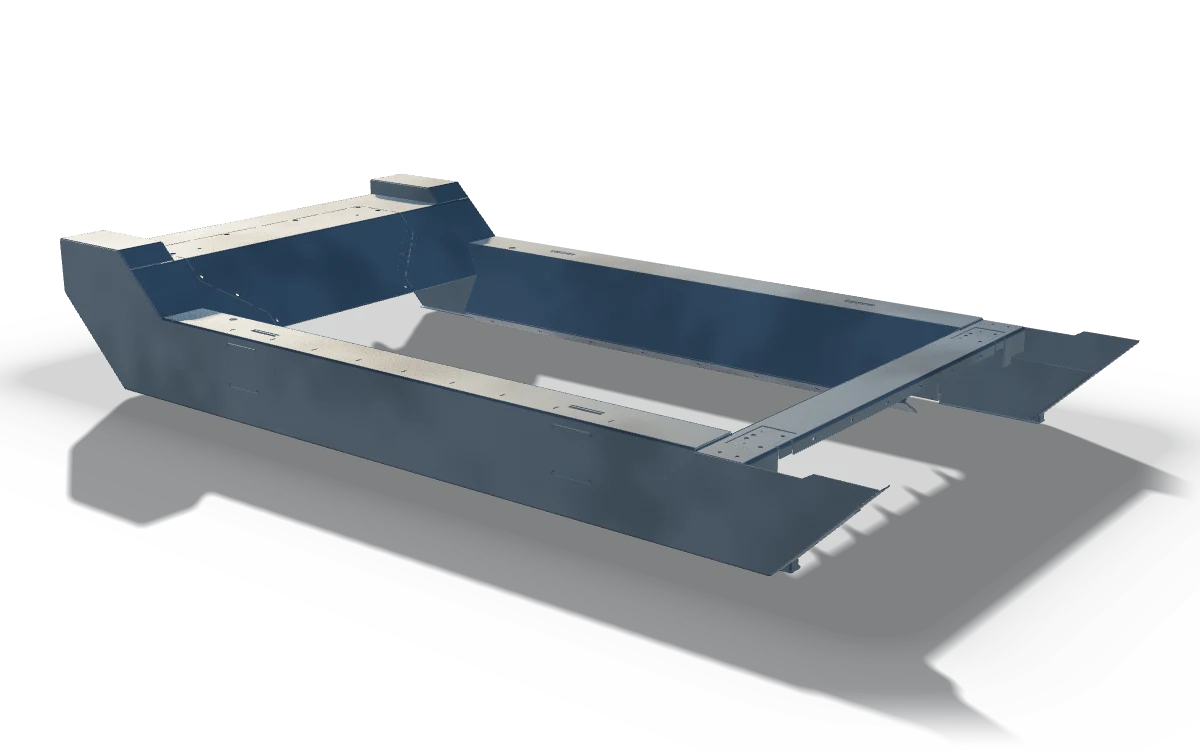
From the shop
Feed hopper, 4.9 m
4 888 x 2 500 x 755 mm

The machine
TRUMPF TruLaser 3040, 3 200 W, cutting to 20 mm. Bend reliefs, locating tabs and weld preparation come off the machine in the blank rather than being added by a fitter.
Photograph published by TANAX TRUCKS a. s. on tanaxtrucks.com. Same company, same hall, our own material; no stock photography is used anywhere on this site.
What it is used for
- Plate parts for weldments: webs, flanges, gussets, end plates, stiffeners
- Hopper walls, cones and transitions folded from cut blanks
- Housing and enclosure panels with folded returns and cut-outs
- Bent brackets, channels and edge profiles for platforms and walkways
- Bolt patterns, slots and lightening holes cut in the nest, not drilled afterwards
What it does not cover
- Plate above 20 mm by laser: heavier plate is sourced pre-cut, confirmed per enquiry
- Blanks larger than the 2 000 x 4 000 mm bed in one piece
- Folds longer than the 6 050 mm table in one hit
- Tube and section laser cutting, plasma and oxy-fuel cutting: not published, ask in the enquiry
- Plate rolling and section rolling: not published, ask in the enquiry
Anything not listed is quoted per enquiry, with the drawing.
What it means for you
Cutting and forming decide what the rest of the part costs. A blank that comes off the laser with its bend reliefs, its locating tabs and its weld preparation already in it goes together in a jig without a fitter making it fit, and that is where the hours are.
It also decides what is possible. A 2 000 x 4 000 mm bed and 6 050 mm between the press brake housings are hard limits on a single piece; longer parts are made in sections with a joint the drawing has to allow. Say early if a joint is not acceptable, because it changes the design and not just the price.
The standards that apply
Cutting and forming are governed by the execution standard rather than by a certificate of their own.
- EN 1090-2, execution class EXC2: the standard that sets what a cut face and a cold formed edge have to be
- EN ISO 9013: the thermal cutting quality classes EN 1090-2 refers to; the class is agreed on the drawing
- EN ISO 13920: general tolerances for welded constructions, class agreed on the drawing
- Plate and section are bought to their own product standards and their certificates are passed through
- No cutting or forming certificate of its own is claimed: neither the parent company nor this site publishes one
Published figures
The two machines and their plates, as published by TANAX TRUCKS a. s.
| Item | Machine | Figure |
|---|---|---|
| Laser bed | TRUMPF TruLaser 3040 | 2 000 x 4 000 mm |
| Laser power | TRUMPF TruLaser 3040 | 3 200 W |
| Maximum plate thickness, laser | TRUMPF TruLaser 3040 | 20 mm |
| Press brake force | DURMA AD-S 60400 | 400 t |
| Press brake table length | DURMA AD-S 60400 | 6 050 mm |
| Press brake stroke | DURMA AD-S 60400 | 365 mm |
Figures as published by TANAX TRUCKS a. s. Anything not listed is quoted per enquiry.
Structure groups that rely on it
Every group starts on the laser; the hoppers, the enclosures and the platforms depend on the press brake as well.


Questions about this process
- What is the largest sheet you can cut in one piece?
- The laser bed is 2 000 x 4 000 mm, so that is the largest blank in one piece. Anything longer is cut in sections and joined, which the drawing has to allow for.
- How thick can you cut?
- Up to 20 mm on the TRUMPF TruLaser 3040 at 3 200 W. Thicker plate is bought cut to size or profiled elsewhere and comes into the hall as a finished blank.
- What is the longest bend?
- 6 050 mm, the table length of the DURMA AD-S 60400, at 400 t of press force and 365 mm of stroke. The usable length for a given radius and thickness depends on the tooling, which is confirmed per enquiry.
- Can you work from a STEP file without a drawing?
- For cutting, usually yes: the flat pattern is developed from the model. For anything that is inspected we still need the drawing, because a model carries no tolerances, no weld symbols and no finish.
- Do you nest several parts on one sheet to save material?
- Yes, and it is worth telling us the whole set at enquiry rather than part by part. Nesting a family of parts together is where the material saving on a batch actually comes from.
Anything not answered here is answered by return of email. Send the drawing with the question and the answer comes back against your part rather than in general.
Where this fits
Cutting and forming feed every group in the hall, and they matter most where a part is mostly folded rather than welded.
Start here
Send the drawing. We answer with a price and a date.
STEP, DWG, DXF, PDF or ZIP, up to five files. Your drawings stay private: they are stored outside the web server and read only by our engineers.