
Capabilities
Welding
Manual and robotic MAG welding of group 1 structural steels and austenitic stainless, under a welding quality system certified to EN ISO 3834-2 and coordinated by an International Welding Engineer.
What it is
The process is MAG 135, manual and automated. A dual robotic welding station on a 14 m track handles long, repetitive seams on frames and conveyor structures; a second robotic cell with a 2 008 mm reach takes smaller weldments; manual MIG/MAG bays weld everything a robot cannot reach and every one-off.
The certified scope covers ISO/TR 15608 group 1 steels, the unalloyed and fine-grain structural grades such as S235 and S355, up to 40 mm, and group 8 austenitic stainless steels from 3 to 16 mm. Product standards in the scope include EN 1090-2, EN 12285-2, EN 14015, API 650, AWS D1.1 and AWS D1.3.
Every weld is made to a written procedure specification (EN ISO 15609-1) qualified to EN ISO 15614-1, by welders qualified to EN ISO 9606-1, under a named welding coordinator qualified as IWE. Weld quality is assessed to EN ISO 5817 at the level the drawing or the execution class requires: level C at EXC2 as standard.
From the shop
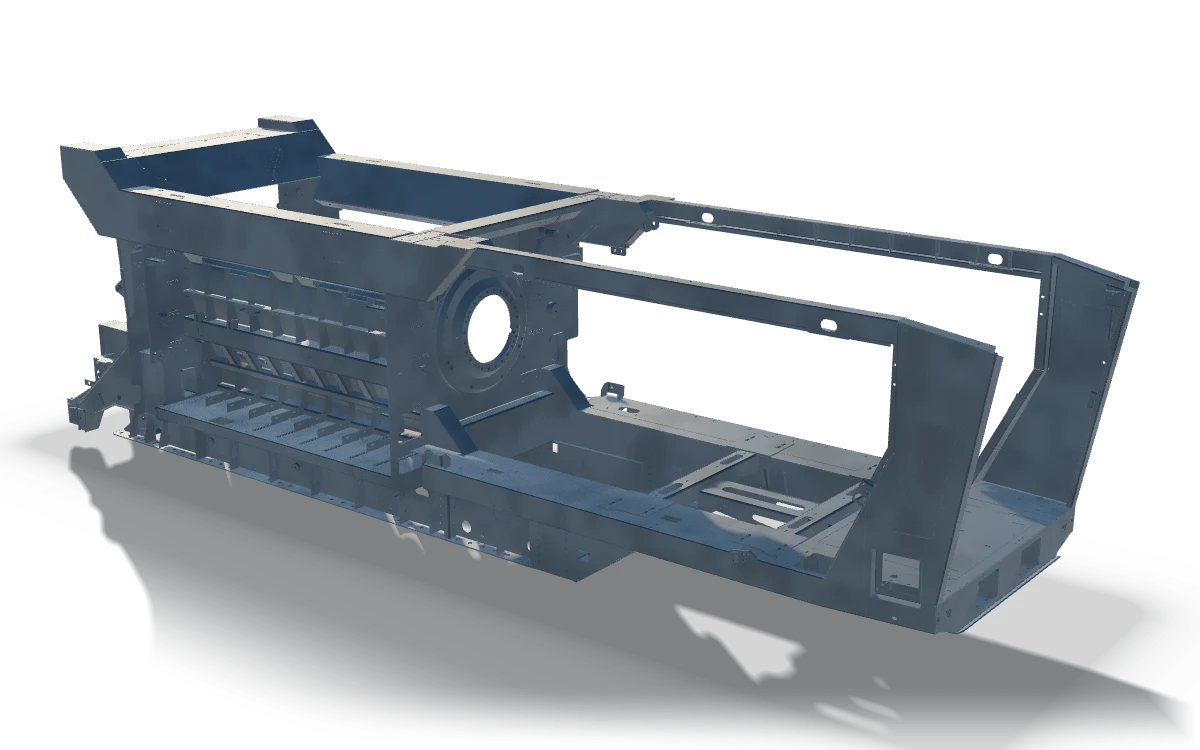
Machine frame weldment, 9.3 m
9 282 x 2 500 x 2 830 mm

The machine
The dual robotic welding station runs on a 14 m track, so a long frame is welded in one setting instead of being turned and re-clamped. That is what makes distortion repeatable across a batch.
Photograph published by TANAX TRUCKS a. s. on tanaxtrucks.com. Same company, same hall, our own material; no stock photography is used anywhere on this site.
What it is used for
- Machine frames, chassis and machine beds in plate and rolled section
- Conveyor and handling structures with long repetitive seams on the robot track
- Atmospheric tanks, hoppers and silos in structural and stainless steel
- Platforms, stairs, handrails and access steel to EN 1090-2
- Housings, guards and enclosures in thin plate, manual and robotic
What it does not cover
- Aluminium: outside the certified welding scope and not offered
- Pressure vessels: the certified scope names atmospheric tanks and structures, not pressure equipment
- EXC3 as a blanket class: EXC3 details on particular joints are agreed at drawing review, not assumed
- An EN 1090-1 factory production control certificate or a CE declaration of performance: not published and not claimed
- Processes other than MAG 135: not published, ask in the enquiry
Anything not listed is quoted per enquiry, with the drawing.
What it means for you
The certificate is the point. EN ISO 3834-2 is not a badge on a wall: it means qualified procedures, qualified welders, a named welding coordinator and records that follow the part. If your own quality system has to audit its supply chain, that is the document that makes this hall auditable.
The robots matter for a different reason. A 14 m track means a long frame is welded in one setting, so the distortion is predictable and repeatable across a batch instead of varying with who welded it. On a one-off it makes little difference; on the fiftieth piece it makes all of it.
The standards that apply
Welding is the one capability here with a certificate of its own, and the whole document list follows from it.
- EN ISO 3834-2, certificate W348721 issued by PQM s.r.o., Banská Bystrica
- EN 1090-2, execution class EXC2, unless the drawing calls for more
- EN ISO 5817, weld quality level C, the level EN 1090-2 assigns to EXC2
- EN ISO 15609-1 for the procedure and EN ISO 15614-1 for its qualification
- EN ISO 9606-1 for welder qualification and EN ISO 17637 for visual testing
- ISO/TR 15608 groups 1 and 8 are the certified material scope; nothing outside them is welded
Published figures
The robotic stations and the certified welding scope, as published by TANAX TRUCKS a. s. and transcribed from the EN ISO 3834-2 certificate.
| Item | Machine | Figure |
|---|---|---|
| Welding process | Manual and robotic | MAG 135 |
| Robotic welding track | Dual robotic welding station, Daihen FD-B6L | 14 m |
| Robot reach | Robotic welding station, Daihen FD-B6L | R 2 008 mm |
| Structural steel, certified thickness (ISO/TR 15608 group 1) | EN ISO 3834-2 scope | up to 40 mm |
| Austenitic stainless, certified thickness (ISO/TR 15608 group 8) | EN ISO 3834-2 scope | 3 to 16 mm |
| Weld quality level (EN ISO 5817) | EN 1090-2, EN ISO 5817 | level C at EXC2 |
Figures as published by TANAX TRUCKS a. s. Anything not listed is quoted per enquiry.
Structure groups that rely on it
Welding is the one capability every group runs through; the groups differ in what is welded and what happens before and after.


Questions about this process
- Are you certified to EN 1090-1?
- No. TANAX TRUCKS a. s. publishes no EN 1090-1 factory production control certificate, so no CE marking and no declaration of performance is issued for a construction product. EN 1090-2 appears as a product standard inside the EN ISO 3834-2 scope, and that is what the execution follows.
- What weld quality level do you work to?
- Level C to EN ISO 5817, which is what EN 1090-2 assigns to execution class EXC2. A drawing can call for level B, and then it is quoted as level B with the extra testing that goes with it.
- Can you weld stainless steel?
- Austenitic stainless from 3 to 16 mm, which is ISO/TR 15608 group 8 on the certificate. Duplex, ferritic and martensitic grades are outside the certified scope and are not welded here.
- Can you weld aluminium?
- No. Aluminium is outside the certified welding scope and is refused rather than welded off certificate.
- Do the welding procedures come with the part?
- Yes. The procedure specifications and their qualification records ship as standard, together with the welder qualifications; nothing has to be asked for.
Anything not answered here is answered by return of email. Send the drawing with the question and the answer comes back against your part rather than in general.
Where this fits
Welding is the one process every group runs through, which is why the groups differ in what happens before and after it rather than in the welding itself.
Start here
Send the drawing. We answer with a price and a date.
STEP, DWG, DXF, PDF or ZIP, up to five files. Your drawings stay private: they are stored outside the web server and read only by our engineers.