
Capabilities
Machining
A welded frame is only as accurate as the faces machined on it afterwards. Mounting faces, bores and bearing seats are machined in the same hall the frame was welded in, on horizontal boring mills sized for large weldments.
What it is
Two CNC horizontal boring mills take the weldments: a TOS Varnsdorf WHQ13 with 3 500 x 2 500 x 1 600 mm of travel, a 1 800 x 2 500 mm rotary table rated for 12 000 kg and a 130 mm spindle, and a TOS Varnsdorf WRD15 with 6 200 x 3 000 x 1 600 mm of travel, a 1 800 x 2 500 mm rotary table rated for 16 000 kg and a 160 mm spindle. A W200 HINR horizontal boring mill with 8 000 x 3 000 x 1 500 mm of travel takes the longest frames.
Turned parts come off a MAS Masturn 550i CNC lathe (X 285 mm, Z 890 or 1 590 mm, 550 mm swing over the bed) and an SKIQ 8 CNC vertical lathe (1 100 mm maximum diameter, 765 mm height, 2 500 kg). A KNC 60 gear hobbing machine cuts wheels up to 600 mm in diameter, module 2 to 13, 5 to 120 teeth.
Machining follows welding, so the faces are cut on the finished weldment and not on parts that will move when they are welded. Frames longer than a machine's travel are machined in sections or on the 8 000 mm mill.
From the shop
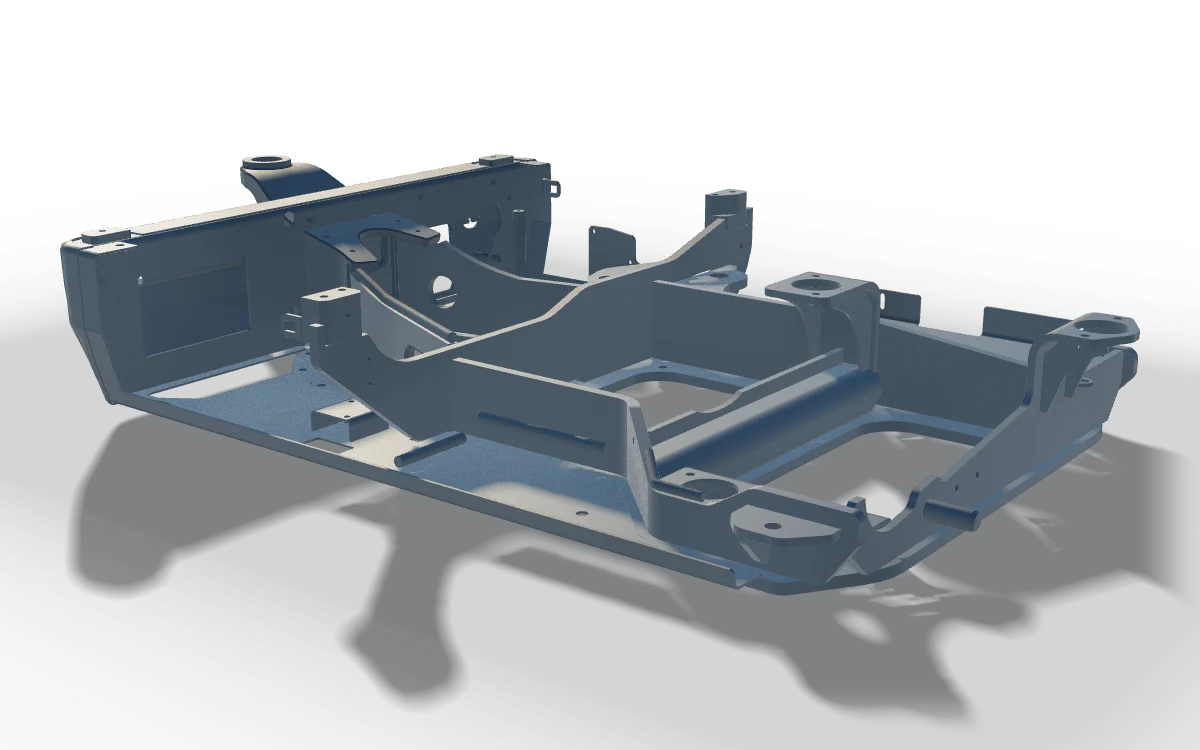
Welded chassis, machined state
1 513 x 982 x 279 mm

The machine
TOS Varnsdorf WRD15, travels of 6 200 x 3 000 x 1 600 mm, a 160 mm spindle and 16 000 kg on the table. The largest machining envelope in the hall.
Photograph published by TANAX TRUCKS a. s. on tanaxtrucks.com. Same company, same hall, our own material; no stock photography is used anywhere on this site.
What it is used for
- Machined mounting faces, pads and bores on welded machine frames and beds
- Bearing seats, gearbox carriers and housing bores true to the frame datum
- Faced flanges and drilled or tapped bolt patterns after welding
- Turned shafts, bushes and rings for our own assemblies
- Gear wheels for welded drive assemblies
What it does not cover
- Five-axis milling, grinding and other processes the parent does not publish: ask in the enquiry
- Machining a face longer than 8 000 mm in one setup
- Rotary-table work above 16 000 kg
- Hardened parts and heat treatment: not published, ask in the enquiry
Anything not listed is quoted per enquiry, with the drawing.
What it means for you
Machining after welding is the difference between a frame and a fabrication. Welding moves steel; a mounting face machined afterwards is flat because it was cut flat, not because the weld happened to leave it that way. If your part has bores that have to line up, this is the capability that decides whether it works.
The travels are the constraint worth checking first. 6 200 x 3 000 x 1 600 mm on the large boring mill and 8 000 x 3 000 x 1 500 mm on the long horizontal mill are the boxes a part has to fit; longer parts are indexed in two settings from one datum, which is normal practice and is stated on the quotation rather than discovered later.
The standards that apply
Machining here is a step inside a welded fabrication rather than a separate service, so the standards that govern it are the fabrication's.
- EN ISO 13920: general tolerances for welded constructions, class agreed on the drawing
- Machining tolerances are taken from the drawing; where a drawing states none, we ask rather than assume
- Datums are taken from the drawing, and the same datum is used for machining and for inspection
- FARO Arm Prime 10 measurement against the drawing where a report is required
- ISO 9001:2015, certificate Q648721, covers engineering production including this work
Published figures
Every machine and its travels, as published by TANAX TRUCKS a. s.
| Item | Machine | Figure |
|---|---|---|
| Horizontal boring mill travel X, Y, Z | TOS Varnsdorf WRD15 | 6 200 x 3 000 x 1 600 mm |
| Rotary table and load | TOS Varnsdorf WRD15 | 1 800 x 2 500 mm, 16 000 kg |
| Spindle diameter | TOS Varnsdorf WRD15 | 160 mm |
| Horizontal boring mill travel X, Y, Z | TOS Varnsdorf WHQ13 | 3 500 x 2 500 x 1 600 mm |
| Rotary table and load | TOS Varnsdorf WHQ13 | 1 800 x 2 500 mm, 12 000 kg |
| Spindle diameter | TOS Varnsdorf WHQ13 | 130 mm |
| Horizontal mill travel X, Y, Z | W200 HINR horizontal boring mill | 8 000 x 3 000 x 1 500 mm |
| CNC lathe travel | MAS Masturn 550i CNC lathe | X 285 mm, Z 890 / 1 590 mm |
| CNC lathe swing | MAS Masturn 550i CNC lathe | 550 mm over bed, 350 mm over cross slide |
| Vertical lathe, maximum diameter | SKIQ 8 CNC vertical lathe | 1 100 mm, table 800 mm |
| Vertical lathe, maximum height and mass | SKIQ 8 CNC vertical lathe | 765 mm, 2 500 kg |
| Gear hobbing, maximum wheel diameter | KNC 60 gear hobbing | 600 mm |
| Gear hobbing, module | KNC 60 gear hobbing | m 2 to 13, currently 5.5 to 6.5 |
| Gear hobbing, tooth width and count | KNC 60 gear hobbing | 110 mm, 5 to 120 teeth |
Figures as published by TANAX TRUCKS a. s. Anything not listed is quoted per enquiry.
Structure groups that rely on it
The groups whose route through the hall includes a machining step: machine frames as a rule, one-offs when the drawing asks for it.


Questions about this process
- What is the largest part you can machine?
- The travels are 6 200 x 3 000 x 1 600 mm on the TOS WRD15 and 8 000 x 3 000 x 1 500 mm on the W200 HINR. Table load is 16 000 kg on the WRD15 and 12 000 kg on the WHQ13. Anything larger than the travel is machined in two settings from one datum.
- Can you machine a frame after it has been welded?
- Yes, and for machine frames it is the usual route: weld, stress relieve if the drawing calls for it, then machine. It is the reason the boring mills and the welding bays are in the same hall.
- Do you cut gears?
- Up to 600 mm diameter on the KNC 60, module 2 to 13 by capability, currently tooled for 5.5 to 6.5, tooth width to 110 mm and 5 to 120 teeth. A module outside the tooled range means new tooling, which is quoted separately.
- What general tolerance do you work to when the drawing does not say?
- We ask. A general tolerance that neither party stated is the most common cause of an argument over a first article, so it is settled at quotation rather than at inspection.
- Can you machine a part we send in already welded?
- Yes. It is quoted as machining alone, and the quotation says what it assumes about the incoming part, because a distorted weldment can take more stock than the drawing leaves.
Anything not answered here is answered by return of email. Send the drawing with the question and the answer comes back against your part rather than in general.
Where this fits
Machining follows welding for frames and weldments, and it is what makes a fabricated part interchangeable with the last one.
Start here
Send the drawing. We answer with a price and a date.
STEP, DWG, DXF, PDF or ZIP, up to five files. Your drawings stay private: they are stored outside the web server and read only by our engineers.